High-purity liquid golden syrups, refined fructose-glucose nectar matrixes, and specialty sweeteners packaged for transpacific bulk shipment and seamless Chilean customs clearance.
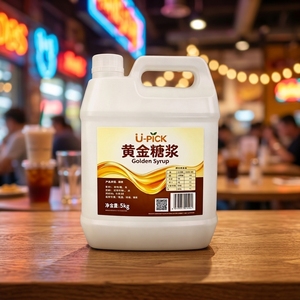
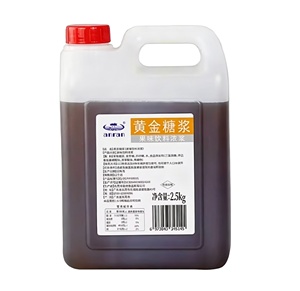
The Chilean food processing and beverage sector represents one of the most sophisticated, highly regulated, and rapidly modernizing markets in Latin America. Driven by strict consumer protection standards under the Ministerio de Salud (MINSAL) and the rigorous requirements of the Reglamento Sanitario de los Alimentos (RSA), food manufacturers operating in Santiago, Concepción, Valparaíso, and the agricultural processing hubs of the Maule and O'Higgins regions demand raw sweetener ingredients that deliver uncompromising technical consistency, high functional performance, and absolute compliance with international purity standards.
Golden syrup—a concentrated, highly refined partially inverted sugar syrup characterized by its golden hue, warm caramel-like flavor profile, and unique anti-crystallization properties—has established itself as an indispensable functional ingredient across Chile's industrial baking, confectionery, canned fruit, artisanal sauce, and booming specialized beverage sectors. Unlike standard liquid sucrose or unrefined molasses, golden syrup provides a balanced blend of sucrose, glucose (dextrose), and fructose. This specific carbohydrate breakdown creates a synergistic humectant effect, depresses the water activity ($a_w$) in baked goods, enhances Maillard browning reactions at lower thermal thresholds, and guarantees zero sugar crystallization throughout a product's shelf life under diverse storage conditions.
As leading international Golden Syrup Manufacturers & Exporters targeting the Chile market, our engineering and supply chain operations are precisely tuned to solve the specific formulation and logistical challenges faced by Chilean importers, procurement officers, and master food technologists. From complying with strict Chilean food labeling laws (Ley de Etiquetado de Alimentos N° 20.606) to maintaining stable viscosity through maritime transit across Pacific trade routes, our global export division delivers factory-direct, certified golden syrup variants tailored for industrial-scale deployment.
Superior humectancy via equimolar glucose-fructose ratios, preventing starch retrogradation and extending soft-baked goods shelf life across Chile's varied climate zones.
Controlled invert ratio ensures zero sugar graining or precipitation in high-Brix formulations, preserving smooth texture in confectioneries and toppings.
Imparts subtle buttery, caramelized flavor notes and golden amber hues without requiring synthetic colorants or artificial masking agents.
To meet the exact processing parameters required by Chilean quality control laboratories and automated manufacturing lines, our golden syrup range is produced under strict acid-catalyzed or enzymatic inversion of food-grade sucrose, followed by multi-stage decolorization, vacuum concentration, and fine filtration. Below is the technical specification matrix comparing our industrial golden syrup grades with standard sucrose and high fructose corn syrups (HFCS 55):
| Physicochemical Parameter | Standard Refined Golden Syrup | High-Fructose Golden Nectar Base | Liquid Sucrose (77°Bx) | Testing Standard / Method |
|---|---|---|---|---|
| Total Soluble Solids (°Brix) | 79.5°Bx - 82.5°Bx | 70.0°Bx - 75.0°Bx | 76.5°Bx - 77.5°Bx | ICUMSA GS4/3/8-13 (Refractometric) |
| Direct Invert Sugar Content | 48.0% - 56.0% (Dry Basis) | 65.0% - 75.0% (Dry Basis) | < 0.5% | Lane & Eynon Volumetric Method |
| Sucrose Content | 25.0% - 33.0% (Dry Basis) | 15.0% - 22.0% (Dry Basis) | > 99.5% | HPLC / Polarimetric Analysis |
| pH Value (1:1 Dilution) | 4.6 - 5.4 | 5.0 - 6.0 | 6.0 - 7.5 | Potentiometric pH Meter |
| Color Scale (ICUMSA Units) | 2,500 - 4,500 IU (Golden Amber) | 1,200 - 2,200 IU (Light Gold) | < 45 IU (Water White) | ICUMSA Method GS2/3-9 |
| Hydroxymethylfurfural (HMF) | < 35 mg/kg | < 20 mg/kg | N/A | HPLC UV-Vis Detection at 284 nm |
| Sulfated Ash Content | < 0.15% | < 0.10% | < 0.03% | Gravimetric Ashing at 525°C |
| Microbiological Parameters | TAMC < 200 CFU/g | Mold/Yeast < 10 CFU/g | Salmonella Negative | ISO 4833 / ISO 21527 Certified |
Control of Hydroxymethylfurfural (HMF) is a critical quality index for long-distance maritime shipments to South America. Elevated HMF levels indicate excessive heat thermal breakdown during processing or transport, which negatively impacts syrup flavor and introduces harsh caramel bitterness. Our proprietary rapid-chill vacuum evaporation protocol guarantees that every batch shipped to Chilean ports maintains low HMF values (<35 mg/kg), ensuring pristine taste profiles upon arrival.
Golden syrup is far more than a simple sweetening agent; it functions as a structural, textural, and aesthetic workhorse in food processing lines. Below, we examine the primary industrial sector applications in Chile where our golden syrup portfolio provides quantifiable performance advantages over traditional sugars.
Chile boasts one of the highest per-capita bread and biscuit consumption rates in Latin America. In industrial baking facilities across Santiago's industrial rings (Quilicura, Lampa, San Bernardo), maintaining soft crumb structure, crust browning control, and moisture equilibrium is paramount. Replacing 10% to 25% of crystalline sucrose with our Natural Liquid Golden Syrup yields distinct operational gains:
Chilean confectionery heritage centers around traditional sweet products such as Alfajores, soft caramels, and the iconic Manjar (dulce de leche). A recurring challenge for dairy processors and candy makers is sugar crystallization (graininess) during ambient shelf life. Our industrial golden syrup acts as a natural crystallization inhibitor:
By disrupting the crystal lattice arrangement of sucrose molecules, the dissolved glucose and fructose fractions maintain a smooth, velvety mouthfeel throughout extended distribution cycles across Chile's regional retail networks. In caramel and hard candy production, our golden syrup facilitates stable glass-state transitions, preventing cold-flow deformities and sticky surface moisture absorption.
Urban centers such as Santiago, Viña del Mar, and Concepción have witnessed exponential growth in specialized tea shops, ready-to-drink (RTD) fruit teas, and Boba milk tea franchises. Beverage formulators require liquid sweeteners that dissolve instantly in ice-cold liquids, exhibit neutral-to-complementary flavor profiles, and enhance beverage viscosity without creating cloying aftertastes.
Our dedicated beverage series—including the HENGZHI 5kg Golden HFCS Syrup (60-70% Brix) and 25KG Commercial Golden Fructose Drums—are engineered specifically for modern beverage dispense units and automated milk tea shaker systems. With instant cold-water dispersion, superior stability in acidic fruit tea bases (pH 2.8 - 4.0), and pristine clarity, these syrups maximize operational efficiency for food-service chains and RTD bottlers alike.
Chile's Central Valley (Región del Maule and Región de O'Higgins) is a global hub for fruit harvesting, freezing, and canning. Export-grade canned stone fruits (peaches, cherries, plums) require packing syrups that preserve cell structure, protect fruit color, and balance natural tartness. Utilizing our golden syrup blends in fruit canning syrup formulation enhances osmotic balance, preserving fruit firmness and color vibrancy while preventing sugar cloudiness inside sealed retail cans.
Navigating the Chilean food market requires an in-depth understanding of evolving consumer demands and stringent government regulation. Three major macroeconomic and regulatory trends are reshaping sweetener procurement across Chile today:
Chile was a pioneer in implementing mandatory front-of-pack nutritional warnings ("ALTO EN AZÚCARES", "ALTO EN CALORÍAS"). Industrial food R&D teams in Chile are actively optimizing recipes to reduce total added sugar weight while maintaining perceived sweetness profiles. Because fructose possesses a sweetness intensity approximately 1.2 to 1.7 times higher than sucrose at cold-to-ambient temperatures, substituting standard sugar with our high-fructose golden syrups allows formulators to reduce dry sweetener dosage (in grams) while achieving identical sensory sweetness levels—helping products remain below regulatory thresholds for warning octagons.
Rising labor, energy, and effluent-treatment costs are prompting mid-to-large-size Chilean food factories to convert from dissolving bagged solid sugar to pumping automated liquid sweeteners. Our bulk golden syrup supply solutions—delivered in sterile 275-gallon IBC totes and full flexitanks—allow Chilean plants to eliminate manual bag dumping, sugar dust explosion risks, dissolving heating costs, and batch preparation delays.
Modern Chilean consumers are looking for alternatives to high-intensity artificial sweeteners like aspartame or acesulfame-K. Golden syrup, produced through the natural hydrolysis of pure sugar cane or sugar beet, provides a recognizable, traditional ingredient declaration on retail labels while delivering superior culinary performance.
Partnering with an experienced global sweetener manufacturer ensures your supply chain remains resilient against market volatility, crop shortages, and maritime shipping disruptions. Our enterprise export architecture is engineered specifically for South American import requirements:
Direct liner sailings to major Chilean ports—Puerto de Valparaíso and Puerto de San Antonio—with average ocean transit times of 18 to 24 days, minimizing lead times for factory inventory management.
Every lot includes a comprehensive Certificate of Analysis (COA), Phytosanitary Documentation, Heavy Metal test sheets, Non-GMO verification, and Halal/Kosher certificates compliant with Chilean SEREMI de Salud clearance.
From 5kg food-service pails and 25kg commercial barrels to 250kg steel drums, 1,300kg IBC totes, and 24,000-liter sterile Flexitanks, we support operations of any scale.
Our long-standing raw cane contracts with primary international sugar mills shield our clients from extreme commodity market spikes. Furthermore, our dedicated R&D team works directly with Chilean corporate clients to customize Brix, color ICUMSA, and invert percentage parameters to fit exact factory dosing systems.
Below are authoritative technical answers to common questions raised by Chilean food production executives, QA directors, and import managers when evaluating bulk golden syrup sourcing:
Partner with a proven global golden syrup manufacturer. Connect with our South American export engineering desk to receive comprehensive product specification sheets, lab samples, and ocean freight quotes for Valparaíso and San Antonio.
